steel detailingshop drawingsBIMproject managementfabrication
Steel Detailing and Shop Drawings: Where Fabrication Programmes Are Won or Lost
Most steel delays are not cutting or welding delays. They are approval delays. Here is how the detailing stage really works and how to stop it consuming your float.
Al Saqr Al Ahmar Welding and Blacksmith LLC3 min read
Ask a project manager why a steel package slipped and you will usually hear about the shop. Ask the fabricator and you will hear about approvals. The second answer is more often the correct one.
Cutting and welding are fast, schedulable and largely under the fabricator's control. Detailing sits between the consultant's design and the shop, and it depends on information arriving from parties who do not report to the fabricator. That is where float disappears.
What detailing actually produces
Detailing converts a design — member sizes, forces, layout — into instructions a machine and a fitter can execute. The outputs are:
- A 3D model of the steelwork, increasingly the primary deliverable rather than a by-product.
- General arrangement drawings showing the erected structure, member marks and grid relationships.
- Assembly and single-part drawings — the shop instructions, dimensioned for fabrication.
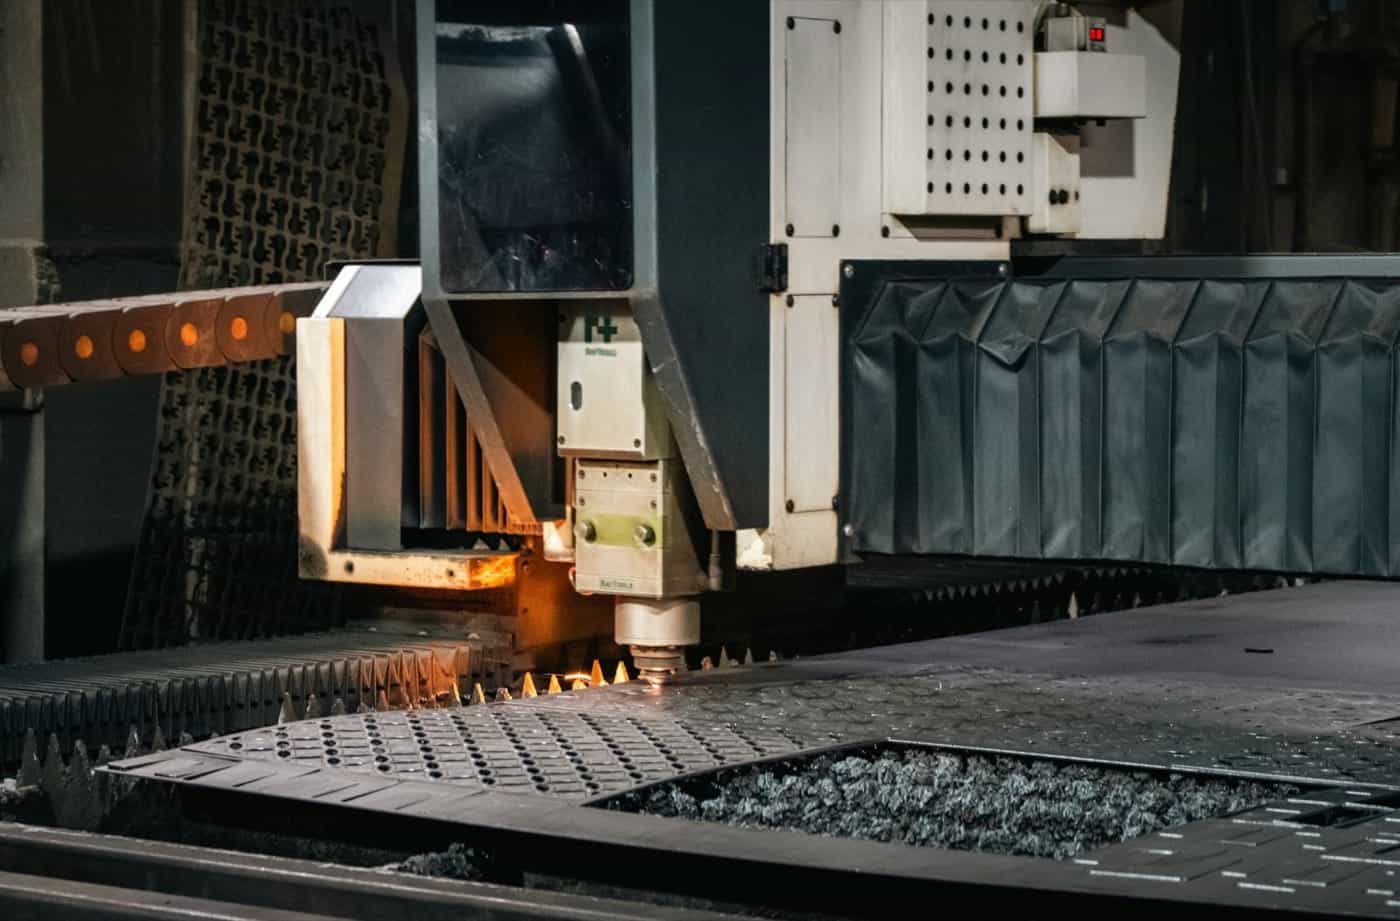
- CNC data — NC1/DSTV files driving profiling, drilling and cutting equipment directly from the model.
- Material lists and bolt lists that drive procurement.
- Erection drawings and marking plans for the site team.
When CNC data comes straight from the approved model, a whole class of transcription error disappears. That is a large part of the argument for keeping profiling in house.
The approval cycle, honestly described
A typical cycle runs: detailer issues drawings → consultant reviews → comments returned → detailer revises → re-issue → approval. Each pass takes real calendar time, commonly one to two weeks with the consultant, and a package usually needs at least two passes.
Three things quietly add passes:
- Missing inputs. Connection forces not shown on the design drawings. Holding-down bolt layouts not fixed. Cladding, services or equipment interfaces undefined. Each generates an RFI, and each RFI stops that part of the package.
- Late design change. A member size change after detailing has started is not one drawing — it ripples into connections, adjacent members, bolt lists and NC files.
- Unclear approval authority. When two parties both comment and disagree, the detailer waits.
The inputs to fix before detailing starts
This list, agreed at kick-off, removes most of the pain:
- Governing design code and connection design responsibility, in writing.
- Design forces at every connection — axial, shear, moment — or a clear delegation of connection design with the criteria to design to.
- Approved foundation and holding-down bolt drawings.
- Steel grades and any specific impact toughness requirement.
- Erection sequence and any temporary stability requirements.
- Surface preparation and coating system, because it affects fit-up and edge treatment.
- Fire protection system, because shop-applied intumescent changes the handling plan.
- Interface information: cladding fixings, services penetrations, equipment loads and bases.
- The approval turnaround commitment and named approver.
Practical measures that save weeks
Break the package into zones
Do not detail, approve and fabricate the whole structure as one block. Split by zone or by erection sequence so the first zone can be approved and cut while the last zone is still being detailed. This single change usually recovers more programme than any shop-floor improvement.
Hold a model review before drawings are issued
A screen-share walk through the 3D model with the consultant, before formal issue, catches clashes and misunderstandings at a point where fixing them costs nothing. It routinely removes an entire comment round.
Run clash detection against other trades
Steel clashes with ductwork, cable tray and pipe racks far more often than with itself. If the other trades are modelled, detect clashes before fabrication, not on site with a grinder.
Track RFIs with a hard ageing report
An RFI older than a week is a programme risk. Publish the ageing list at every progress meeting — visibility alone changes response times.
Agree tolerances explicitly
Fabrication tolerances and erection tolerances are different, and both need to be compatible with the tolerances of what connects to the steel. Cladding disputes usually trace back to nobody having reconciled the three.
What good looks like
On a well-run package, the fabricator receives complete information, the detailer issues zoned drawings, the consultant turns comments around in a committed window, and the shop receives approved NC data that drives the machines directly. Steel arrives on site marked, in erection sequence, with the right bolts in the right box.
None of that is exotic. It is mostly the consequence of settling a short list of questions before anyone starts drawing.
Al Saqr Al Ahmar handles design, detailing, CNC profiling, fabrication and erection in house from our Musaffah yard, which keeps the model-to-machine path short. See our capabilities or send us a scope.
Keep reading
More from the blog
21 October 2026 · 4 min read
Steel Structure Cost in the UAE: 9 Factors That Decide Your Quotation
What drives the price of a steel building in the UAE, and how to compare fabrication quotations fairly.
21 October 2026 · 1 min read
Pipeline Welding for Onshore and Offshore Oil & Gas: An Overview
A look at what pipeline welding scopes typically involve — components, supports, clamps and pipe racks — and why fabrication quality matters for oil & gas facilities.
21 October 2026 · 1 min read
Why ISO 9001, 14001, 45001 and ADNOC ICV Certification Matter When You Hire a Fabricator
What ISO 9001, ISO 14001, ISO 45001 and ADNOC ICV certification actually verify — and why they should be on your fabricator shortlist checklist.